Coming next · in build now

Every problem caught, fixed at the root, and checked it held.

Audit findings, customer complaints, supplier issues, calibrations out of tolerance, production defects: one log, one way to contain, find the cause, fix it and prove the fix worked.

40 assemblies haveM4×10 screws. Hold them all.I'm raising an NC.
Makkal AIAI already reads calibration certificates in GageMakkal.Every app shares the same rule: AI prepares, a person decides.See Makkal AI →
Prototype: the screens below come from the CapaMakkal prototype, with made-up data.
01

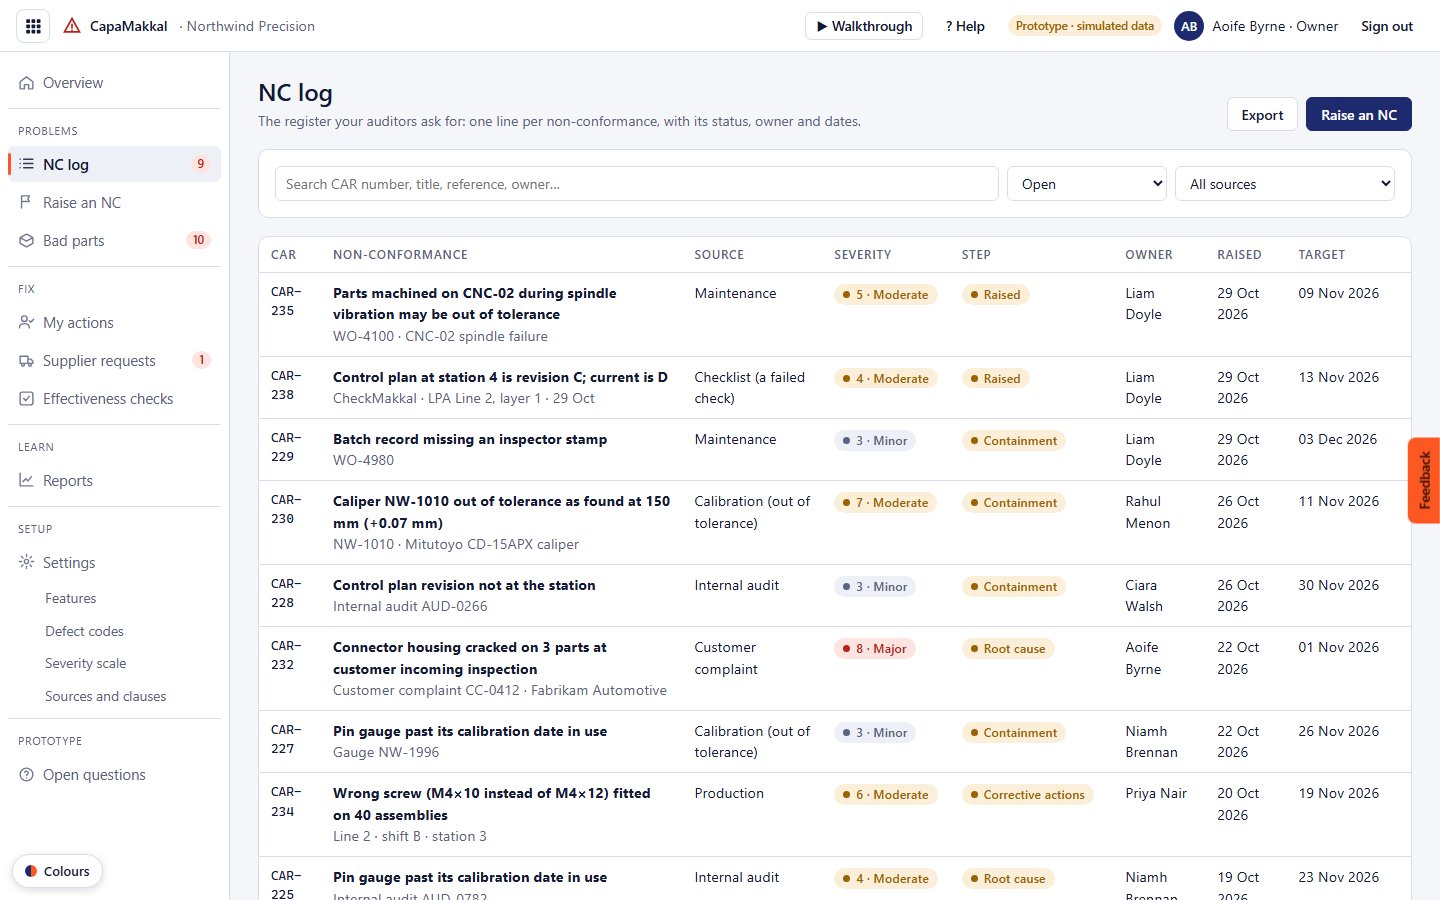
Every non-conformance in one log

  • Raised from an audit, a customer complaint, a supplier, a calibration out of tolerance, production or maintenance.
  • Severity, owner, step and target date on every line: the register your auditors ask for.
  • Raised from a phone on the floor, or from the app the problem came from.
NC log: one line per non-conformance, from every source
02

Contain it, then decide the bad parts

  • Containment first: suspect stock checked and put aside, by whom and when.
  • Bad parts are held until someone decides: scrap, rework or use as is.
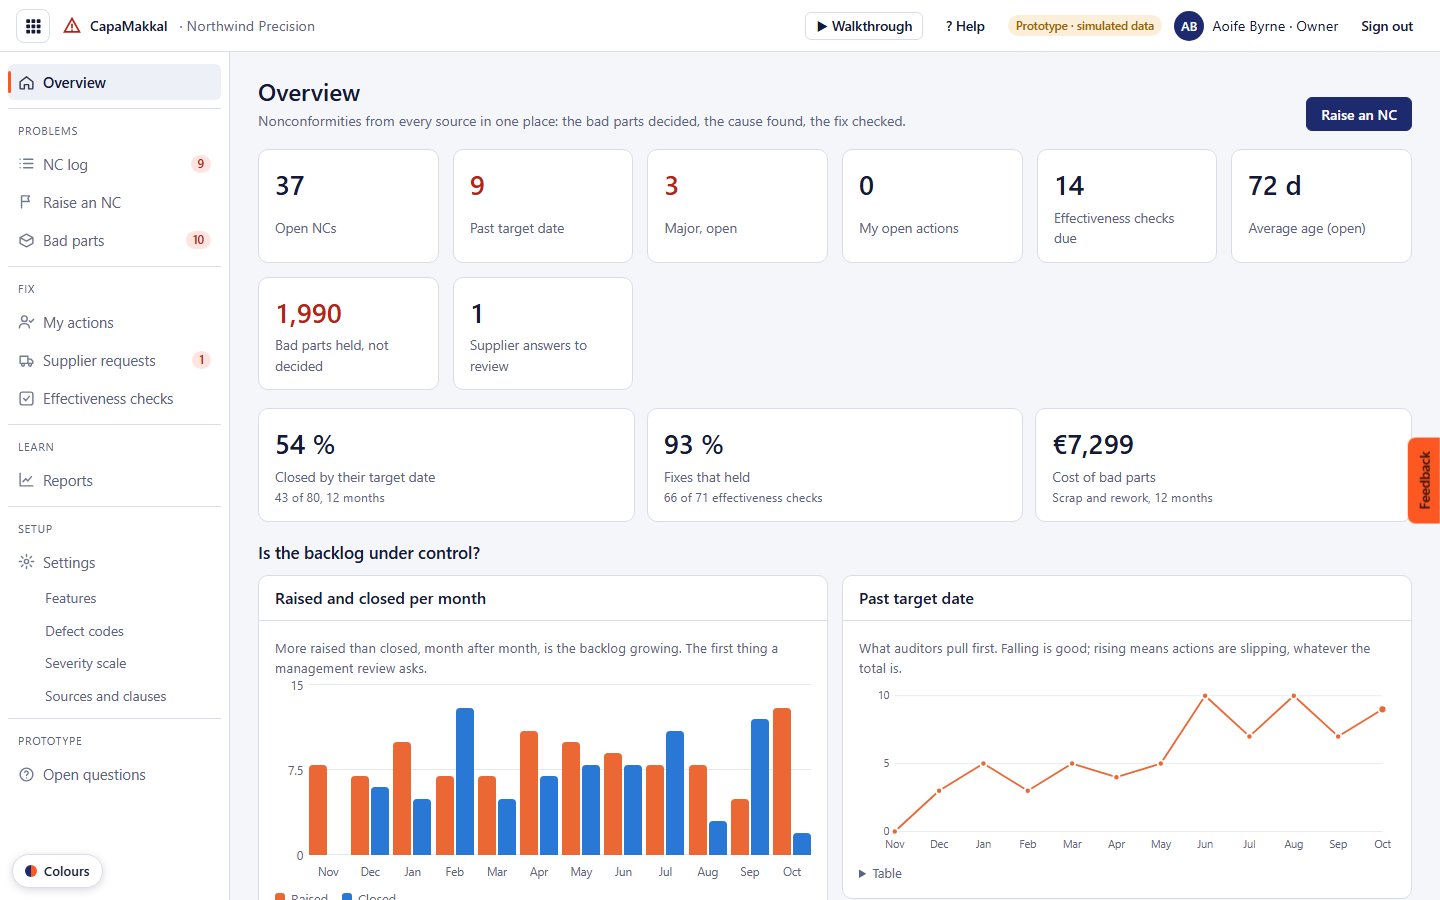
  • The cost of bad parts, and how many NCs closed by their target date.
Overview: open NCs, bad parts held, cost of bad parts
03

The root cause, fixed three ways

  • Five whys to the root cause.
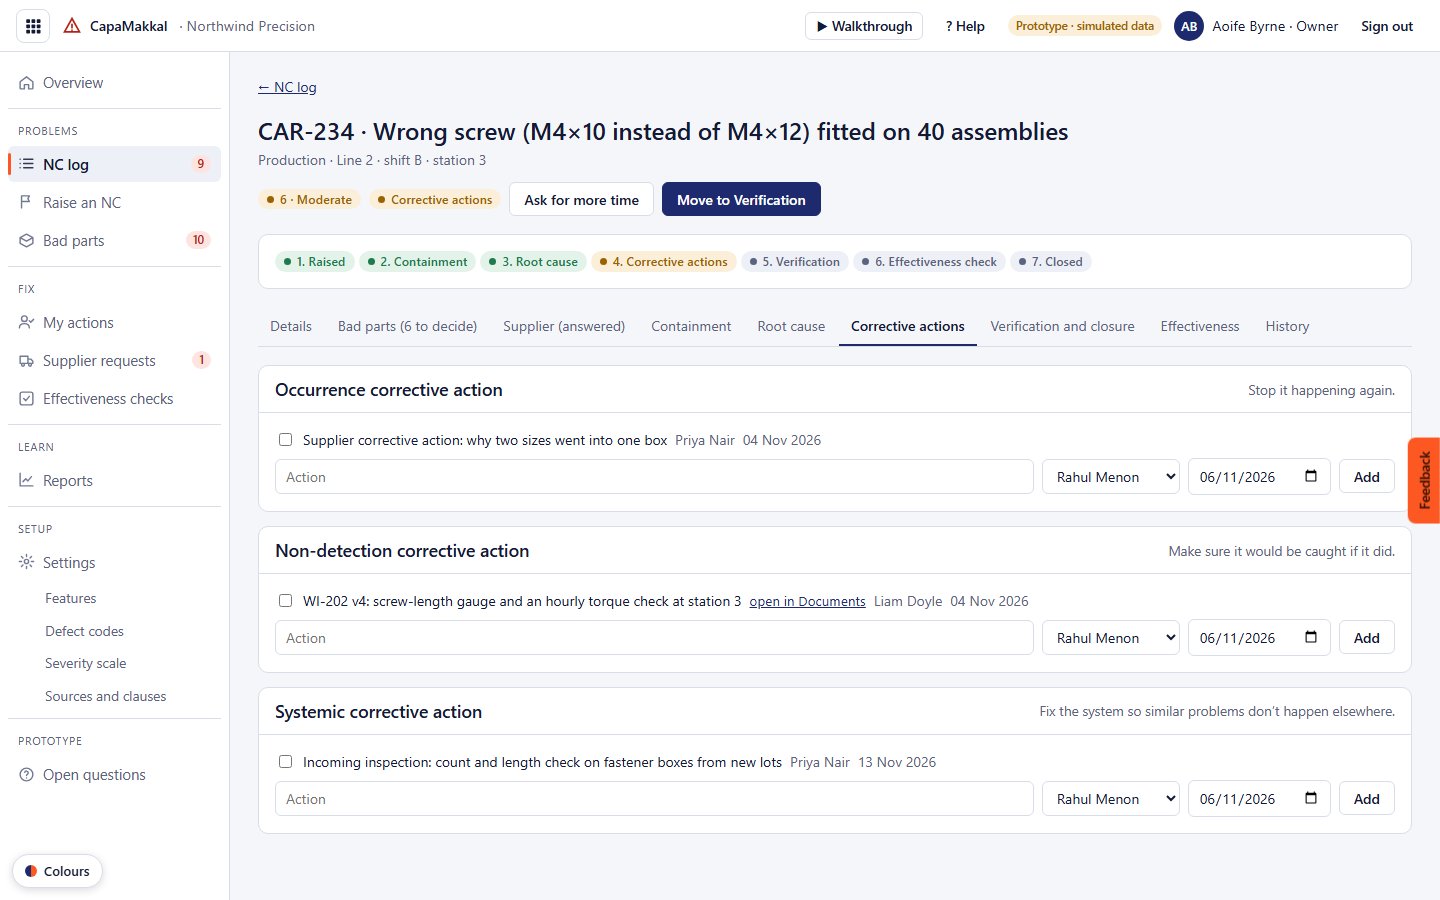
  • Occurrence, non-detection and systemic actions, each with an owner and a due date.
  • Ask a supplier for their answer and see it in the same record.
One NC: its steps, and the three kinds of corrective action
04

Prove the fix held

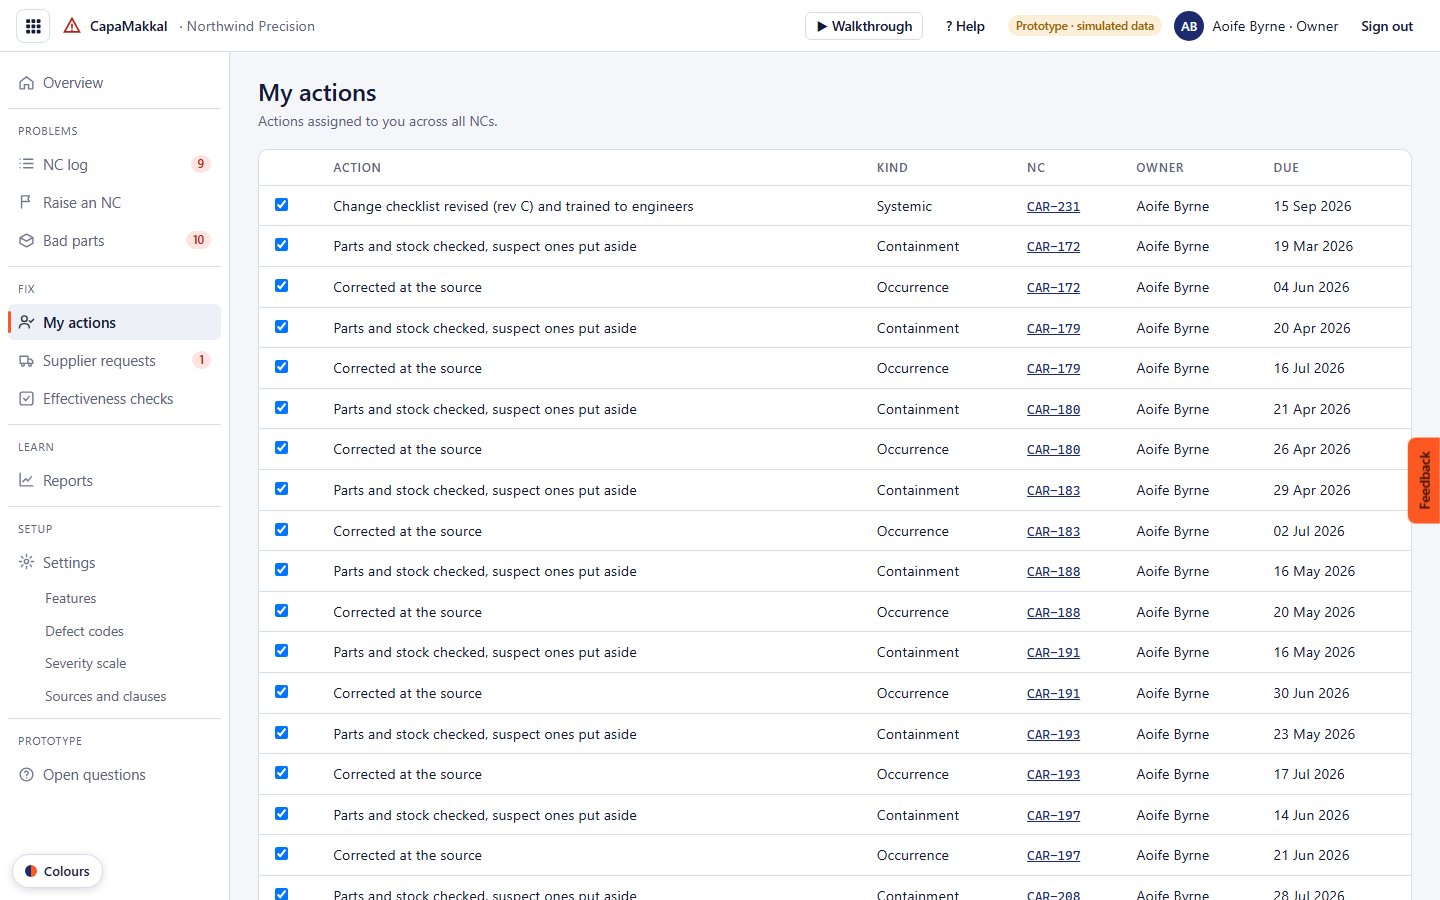
  • Verification and closure with evidence, signed by the person who checked it.
  • An effectiveness check after the time you set; reopen if it did not hold.
  • Reminders before target dates, and extensions only with a reason.
My actions: every action given to you, across all NCs
Line 2, station 3

Wrong screws in 40 assemblies. Thirty days later, it has not come back.

  1. Raise and containPiotr raises it from his phone. Anna holds the 40 assemblies and the stock in the box.
  2. Find the causeFive whys lead to the supplier: two sizes in one box. Their answer comes back into the same record.
  3. Fix and checkA length gauge and an hourly torque check go into work instruction rev 4 in DocuMakkal. After 30 days, Anna checks it held.
Is the screwproblem closed? Closed, and itheld for 30 days.
Works with

Better with the rest of the honeycomb.

Audit findings arrive from AuditMakkal, instructions change in DocuMakkal, calibrations out of tolerance come from GageMakkal, and failed checks from CheckMakkal.

Talk to us early

Shape CapaMakkal before it opens.

CapaMakkal is being built now, with plants like yours. Tell us how you work today and what gets in the way.

  • A person answers within one working day, not a bot.
  • We show you the prototype on a call, with examples from your plant.
  • Early plants decide what comes first, and get it first.
What would you like?

We use your details only to answer you. No newsletter unless you ask.

Be first to close your NCs in CapaMakkal.

Bring your current NC log as a spreadsheet; we'll show you your own problems in it before it opens to everyone.

One email when CapaMakkal opens. Nothing else.